Follow us
Products · Products · Products · Products · Products · Products · Products · Products · Products · Products · Products · Products · Products · Products · Products · Products ·
PPR Fusion Welder

Home · Products · PPR fittings · PPR Insert Fittings · PPR Fusion Welder

PPR Fusion Welder

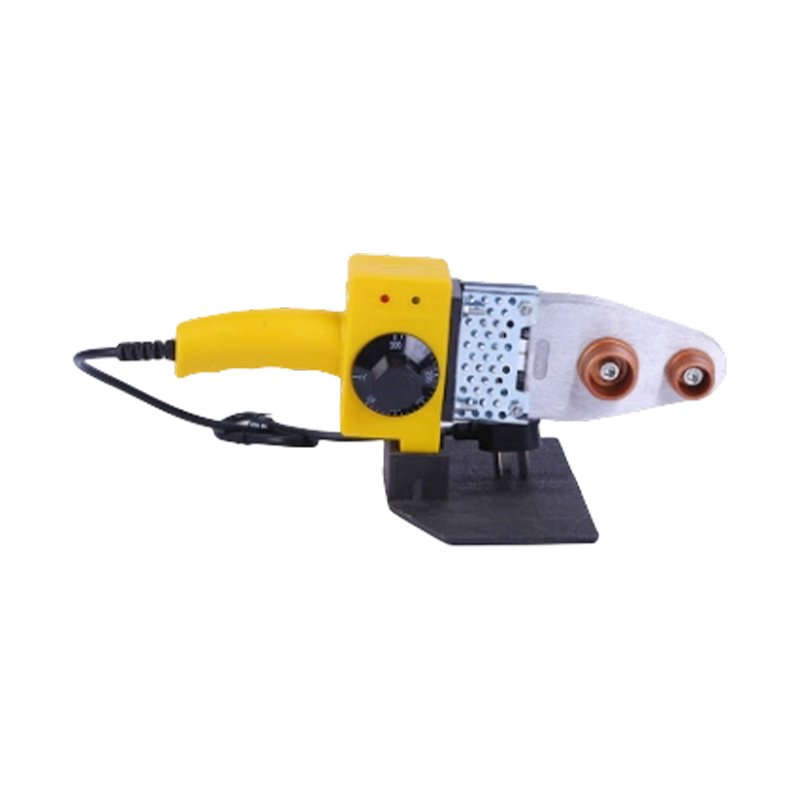
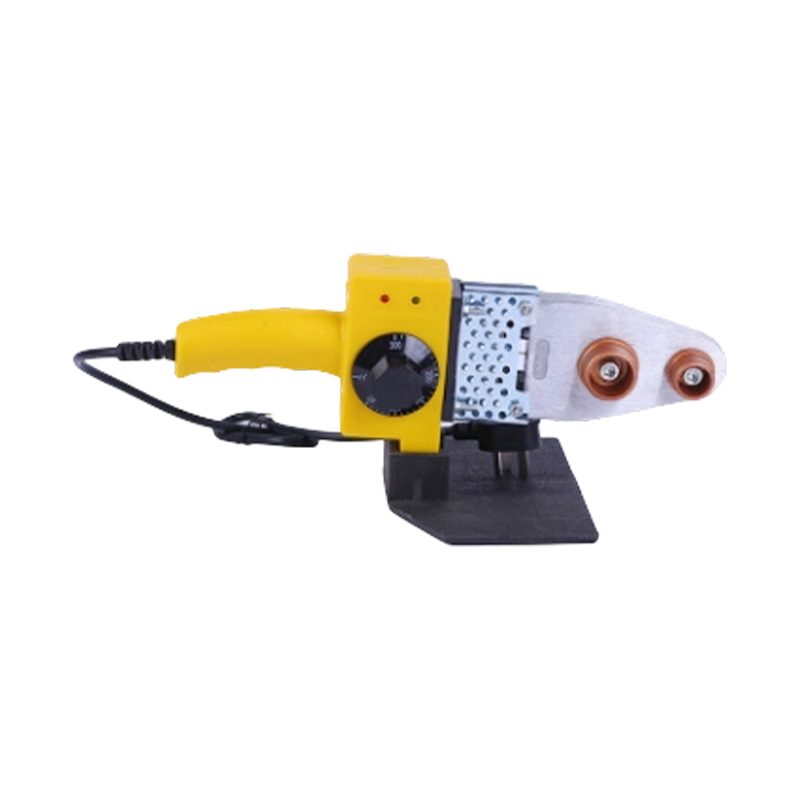
The PPR Fusion Welder is a heat fusion tool used to join PPR (and compatible PE) pipes and fittings by softening the mating surfaces with controlled heat until they can be pressed together to form a single, continuous joint. Rather than relying on adhesives, threads, or mechanical seals, the fused connection becomes structurally part of the pipe itself once it cools, which is why heat fusion is the standard joining method for PPR piping systems used in water supply, heating, and general plumbing installations.
The tool consists of a heating plate fitted with interchangeable sockets sized to match different pipe diameters, available in 20- 32 mm and 20- 63 mm ranges, covering most of the pipe sizes commonly encountered in residential and light commercial plumbing work — from smaller branch lines up to larger main runs. The heating plate reaches and holds a controlled temperature suited to PPR material, allowing the installer to heat the pipe end and the fitting socket simultaneously before joining them by hand within the working time available.

Application Scenarios & Installation

The PPR Fusion Welder is typically used wherever PPR pipe runs are being installed or extended — cold and hot water distribution lines, underfloor heating supply pipes, and general plumbing branches in residential buildings, as well as larger installation runs on commercial and hospitality projects. The 20-32mm range is generally suited to smaller branch and fixture supply lines, while the 20-63mm range covers larger main distribution runs and heavier-duty installation work. The tool is also commonly kept on hand for repair work, where a damaged section of PPR pipe needs to be cut out and rejoined with new fittings.
Because the strength of a fused joint depends on consistent heat and correct timing, installers generally prepare the pipe ends (cutting square, cleaning, and marking insertion depth) before heating, and aim to complete the heating and joining steps within the timeframes recommended for the pipe diameter being worked with — shorter for smaller sizes within the 20-32mm range, and correspondingly longer for larger diameters up to 63mm. Once joined, the connection is typically left undisturbed for a short cooling period before the line is pressurized or covered, since disturbing a joint before it has fully set can weaken the fusion.


NAME SIZE RMB(UP) Box gauge
PPR Machine 20-32 Hot Melt Applicator 50 49*24.5*24.5
20-63 Hot Melt Applicator 58 49*24.5*24.5